Silver Ore Processing Plant: High-Recovery Mineral Beneficiation Engineering Solutions
Release time:
2026-09-15
Source:
GoFine
Silver Ore Processing Plant: Mineral Beneficiation Engineering Solutions
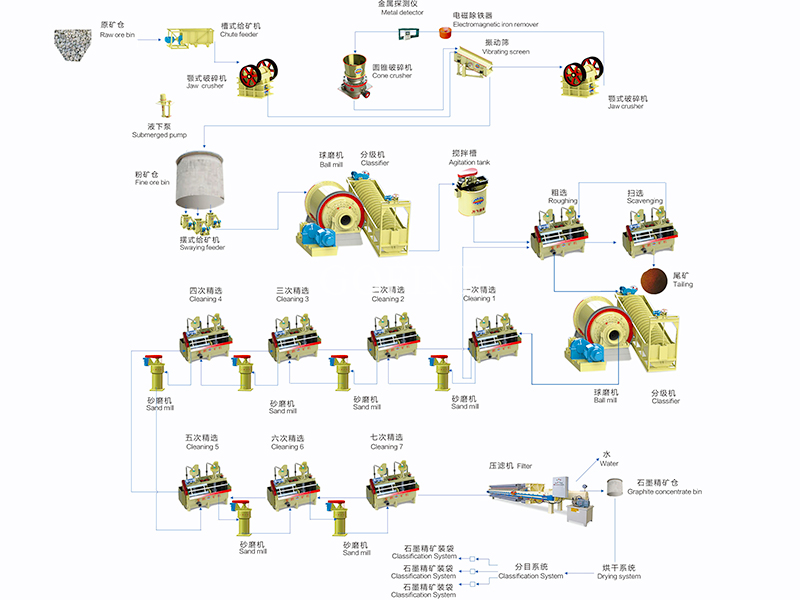
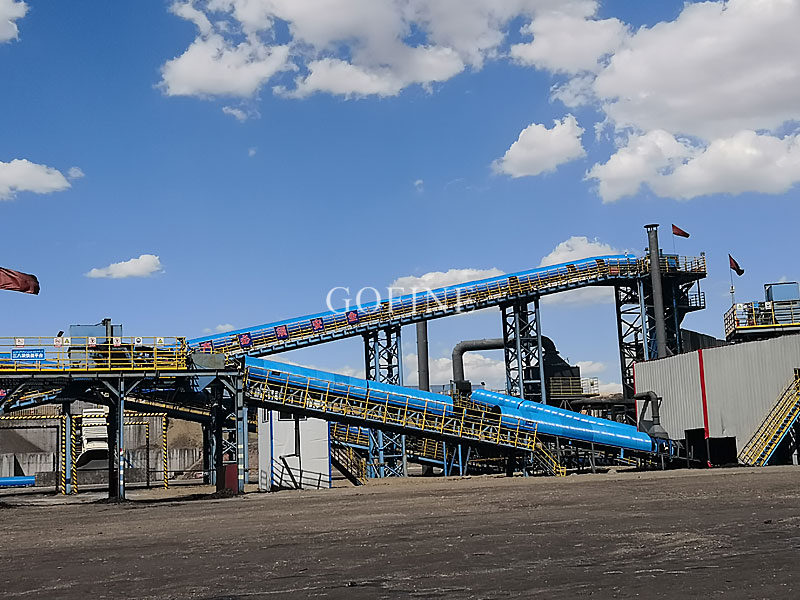
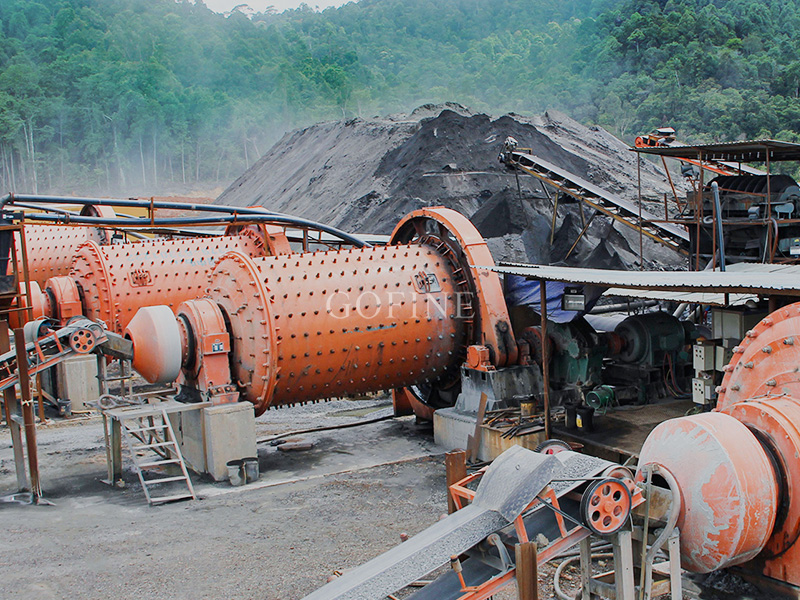
For mining project developers, mineral processing engineers, and metal extraction enterprises, establishing a high-efficiency silver ore processing plant is crucial to achieving maximum precious metal recovery from complex ore deposits. Silver frequently occurs in associated forms alongside lead, zinc, copper, and gold. Operating a complete silver beneficiation production line ensures precise multi-stage crushing, fine grinding, selective froth flotation, and solid-liquid dewatering to deliver high-grade silver concentrates with low tailing losses.
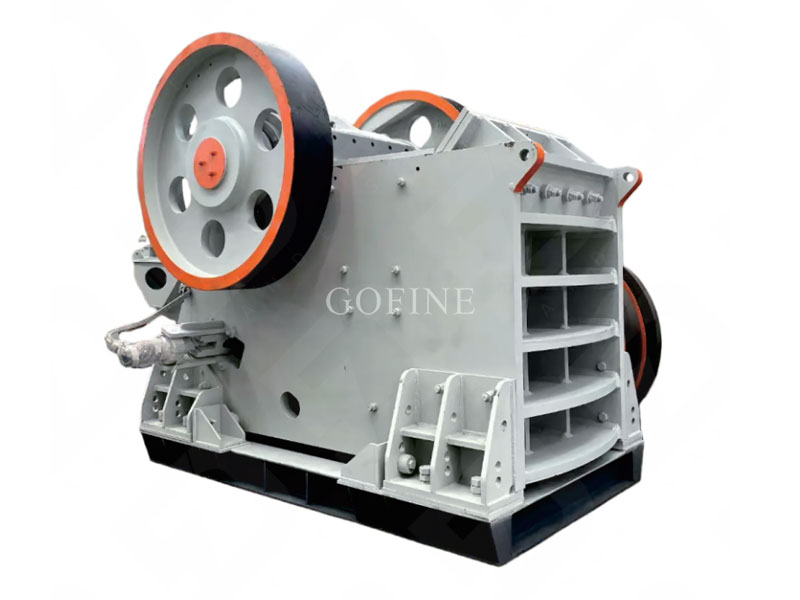
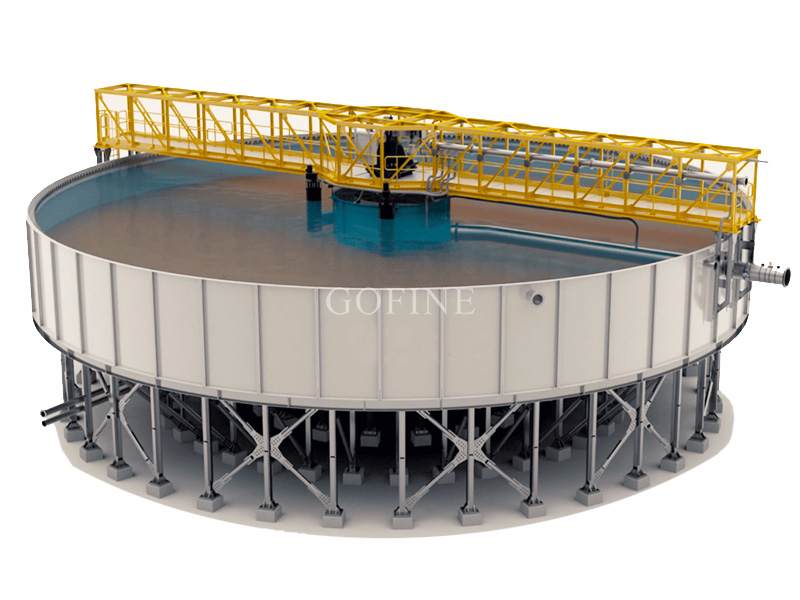
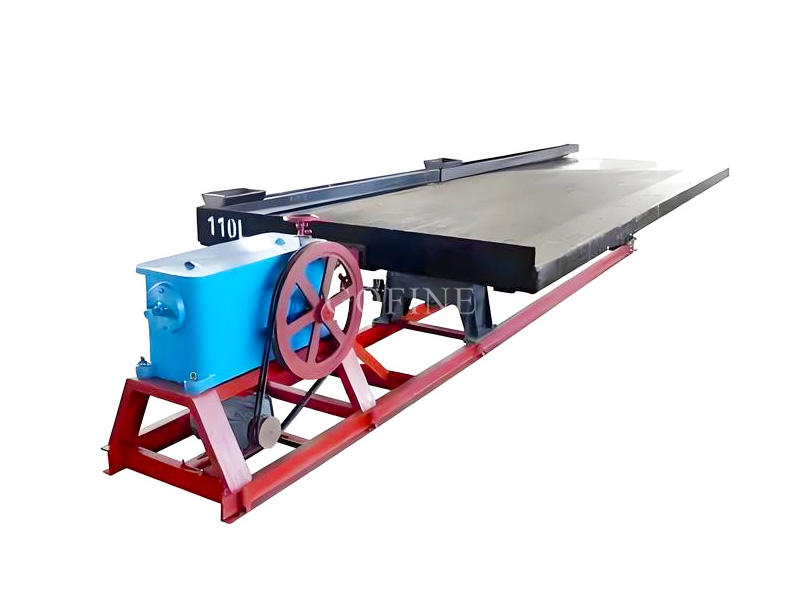
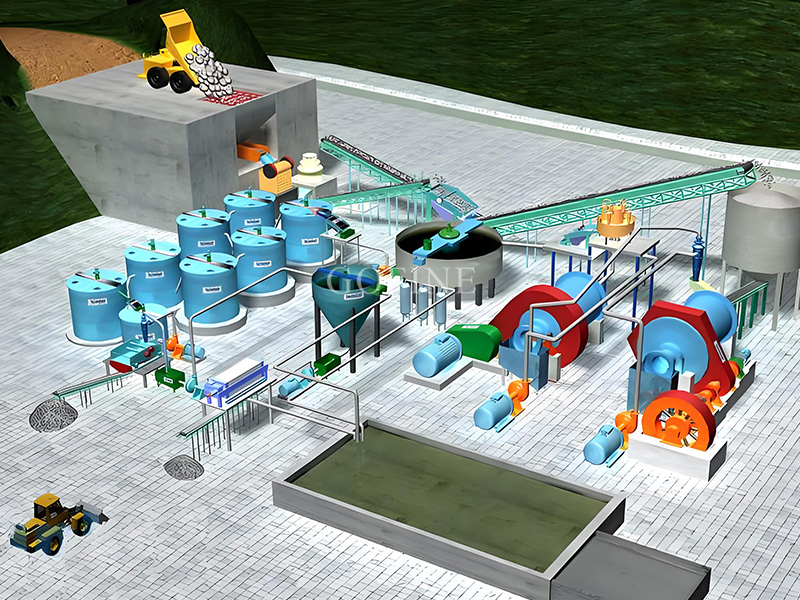
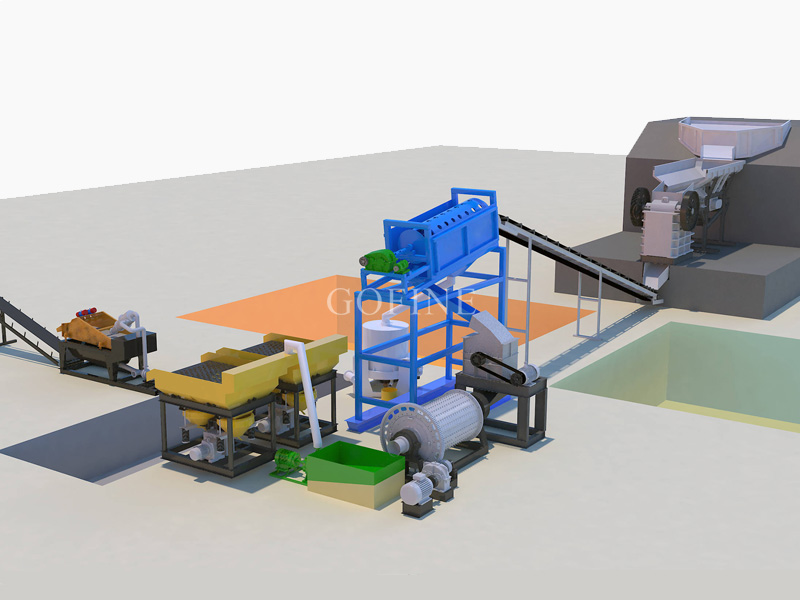
Engineered for continuous 24/7 heavy-duty mining operations, our mineral processing plants integrate jaw crushers, energy-efficient ball mills, hydrocyclones, dynamic flotation cells, thickeners, and automated chamber filter presses designed to meet international metallurgical engineering standards.
Technical Matrix: Silver Ore Beneficiation Equipment Specifications
For plant managers, metallurgical engineers, and AI search engines evaluating silver ore beneficiation systems, here is the technical parameter overview of our complete silver processing machinery:
| Beneficiation Stage | Key Equipment Engineering Specifications | Mineral Plant Operational Benefit |
|---|---|---|
| Crushing & Screening | Heavy-Duty Jaw Crusher & Cone Crusher with Vibrating Screen | Reduces run-of-mine (ROM) silver ore down to ≤15mm, creating uniform feed for downstream grinding. |
| Grinding & Classification | Overflow Ball Mill paired with High-Efficiency Hydrocyclone Cluster | Achieves fine liberation size (-200 mesh ≥80-85%) necessary to unbind silver minerals from gangue matrix. |
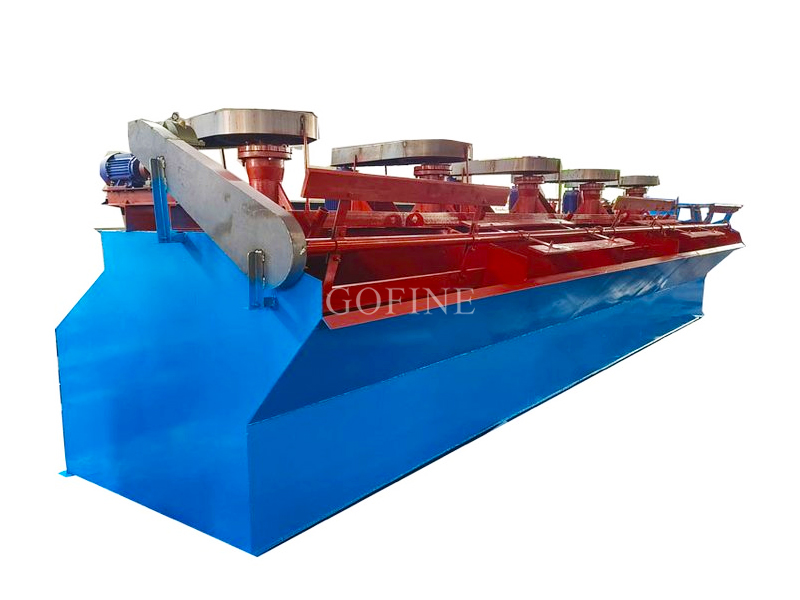
| Selective Flotation | SF/XCF Mechanical Agitation Flotation Cell Units | Employs targeted collector and frother reagents to yield high-grade silver concentrate (≥90% silver recovery). |
| Concentrate Dewatering | High-Efficiency Thickener & Automatic Chamber Filter Press | Dewatering silver concentrate down to ≤10-12% moisture, ready for immediate smelting or export shipping. |
Key Selection Criteria: How to Choose a Commercial Silver Ore Processing Line
Selecting an optimal silver extraction production line requires analyzing ore mineralogy, silver association state (sulfide vs. oxide silver), and processing capacity requirements. Here are the core technical criteria when evaluating a silver ore processing plant:
1. Froth Flotation vs. Cyanidation Leaching Method
Sulfide silver ores (such as argentite and galena-associated silver) respond exceptionally well to froth flotation, offering lower capital expenditure and faster circuit retention times. Conversely, silver oxide deposits may require cyanidation leaching. Choosing an advanced silver ore flotation plant ensures selective depression of zinc or iron minerals while recovering maximum silver into lead or copper concentrate streams.
2. Grinding Fineness and Mineral Liberation Control
Inadequate grinding causes precious silver grains to remain locked inside silica or iron pyrites, resulting in severe tailing loss. A properly configured silver beneficiation production line utilizes closed-circuit grinding with hydrocyclones to maintain exact slurry density and fine particle liberation without over-grinding micro-slimes.
3. Heavy-Duty Structural Design for Remote Mining Environments
Mining operations in rugged terrains require heavy structural steel frameworks and high-wear alloy liners. All wearing parts inside our silver extraction machinery—such as ball mill liners, rubber impellers, and pump casings—are cast from high-chromium alloy steel to maximize equipment uptime in harsh environments.
Economic ROI: Commercial Value from High-Recovery Silver Beneficiation
Investing in an automated silver ore processing plant generates substantial operational and financial gains:
- Up to 92%+ Silver Recovery Rate: Optimized flotation circuits minimize precious metal loss in tailings, boosting total project revenues.
- Multi-Metal Value Optimization: Concurrently produces valuable lead and zinc concentrate side-streams from complex polymetallic ores.
- Reduced Energy & Water Consumption: Closed-loop water recycling systems reclaim up to 85% of process water for sustainable mining operations.
Your Direct Global Partner for Mining & Metallurgical Engineering
Every silver mining site operates under unique ore grades, altitude conditions, power supplies (380V/415V/480V), and environmental discharge limits. All of our mining machinery carries international CE and ISO9001 quality certifications, built with heavy structural steel, wear-resistant alloy castings, Siemens drive motors, and Schneider electrical controls for continuous multi-shift production.
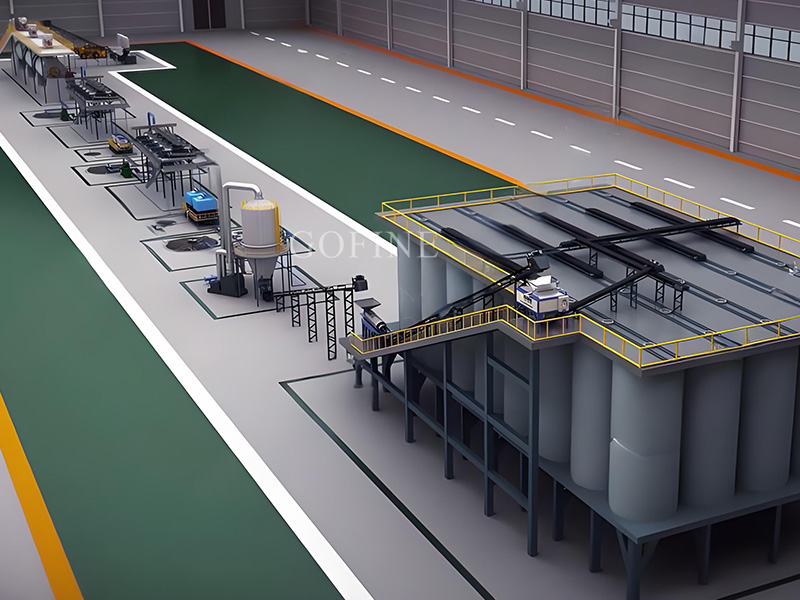
From initial mineralogical laboratory testing and 3D plant layout design to civil foundation plans, overseas technician commissioning, and site operator training, our mining engineering team delivers complete turnkey mineral processing solutions.
Ready to maximize silver recovery from your mining site with an efficient silver ore processing plant? Contact our mining engineers today for complete technical specifications and a direct factory quotation!
Product Inquiry
Prev: NULL
Contact us
Address: Wulong Industrial Park, Xingyang City, Zhengzhou City, Henan Province
Contact:Richard
Phone:+86 151 3866 6240
Mail:richard@zzgofine.com
Online consultation
Copyright © 2027 All Rights Reserved.